Why Choose Aluminium Dies for Global Manufacturing?
Why Choose Aluminium Dies for Global Manufacturing?
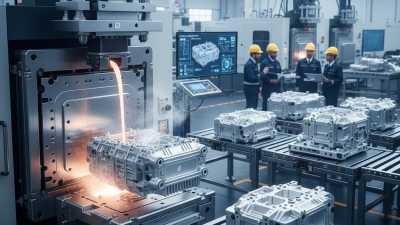
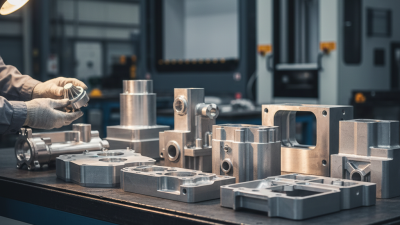
Global manufacturers are rethinking tooling, not merely reducing purchase prices. Aluminium dies offer a practical balance between weight, thermal performance, machinability, and production speed. A large die can move across a workshop floor with less lifting equipment. That difference matters when factories change models frequently.
The International Aluminium Institute projects aluminium demand could rise by almost 80% by 2050. Its research also highlights recycling as a major pathway for reducing future emissions. According to the International Energy Agency, recycled aluminium requires roughly 5% of the energy used for primary production. These figures strengthen the case for Dies Aluminium in industries seeking lighter tools and more circular material flows. However, energy savings depend on collection systems, alloy separation, and efficient remelting. The material alone cannot solve everything.
Casting expert John Campbell famously stated, “The best way to make a good casting is to make a good casting.” His principle applies directly to die design. Accurate wall thickness, controlled cooling, and careful surface finishing influence tool life. Small details matter. A poorly designed aluminium die can deform, wear quickly, or create inconsistent parts. That weakness deserves honest attention.
Still, aluminium tooling remains compelling for prototypes, low-to-medium production runs, and components requiring rapid heat transfer. Its lighter structure can reduce handling strain and shorten changeover time. Global buyers should compare alloy grade, coating, maintenance access, and expected cycle volume before ordering. The strongest decision is not automatically the cheapest one. It is the decision supported by tested performance, transparent data, and realistic manufacturing experience.
Aluminium Die Fundamentals: 2.70 g/cm³ Density and Key Alloy Families
Why Choose Aluminium Dies for Global Manufacturing?
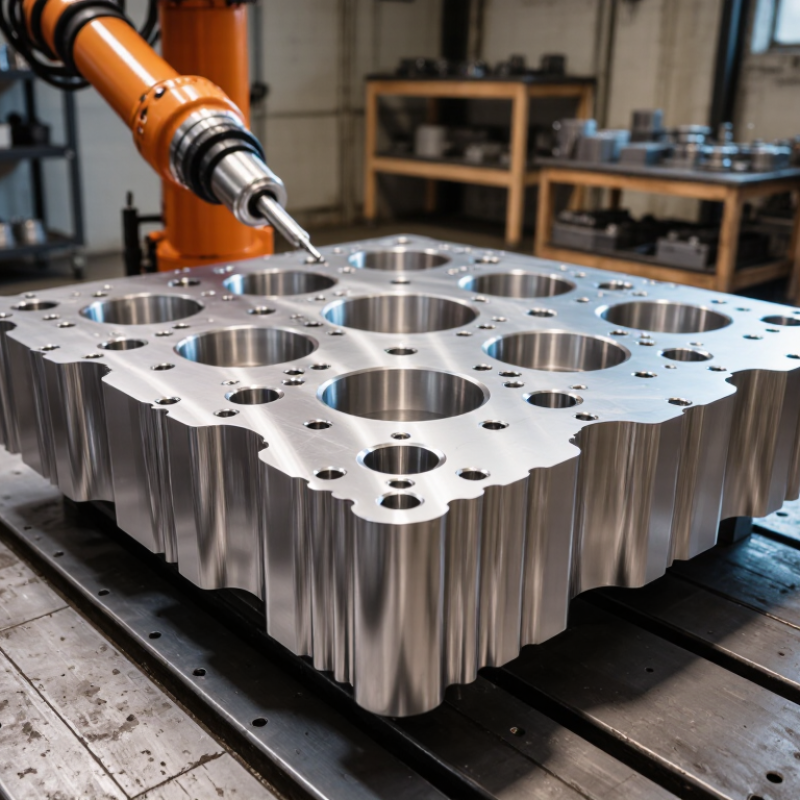
Aluminium has a density of about 2.70 g/cm³, nearly one-third that of steel. This low mass makes die handling easier during installation, maintenance, and transport. A medium-sized die feels noticeably lighter on a shop-floor crane. The International Aluminium Institute reported approximately 70.6 million tonnes of primary aluminium production in 2023. That scale supports broad material availability across global manufacturing regions.
Alloy selection matters more than density alone. Wrought families include 1xxx, 3xxx, 5xxx, 6xxx, and 7xxx series, while common casting families include 2xx, 3xx, 4xx, and 5xx series. Silicon-rich 3xx alloys generally offer strong castability and practical corrosion resistance. Magnesium-containing 5xxx alloys can provide useful strength, but their forming and thermal behavior require careful control. The Aluminum Association’s alloy designations help engineers compare composition and intended performance.
The number is useful, but it can mislead. I would not specify an alloy from density alone. Heat resistance, fatigue life, surface wear, and dimensional stability may change the decision. The U.S. Geological Survey’s Mineral Commodity Summaries identifies aluminium as a major industrial material with extensive recycling flows. Recycled feedstock can reduce material demand, yet quality still depends on sorting and process control. In real production, a lighter die is not automatically a better die. Engineering judgment remains essential.
Why Choose Aluminium Dies for Global Manufacturing?
Aluminium has a low density of approximately 2.70 g/cm³, supporting lightweight tooling and efficient material handling.
Actual density varies by alloy family because of differences in alloying elements such as silicon, magnesium, copper, zinc, and manganese.
The values shown are representative engineering values for common wrought and die-casting alloy groups.
Tooling Efficiency: Aluminium Dies Can Reduce Weight by Nearly 65%
In global manufacturing, tooling weight directly affects handling, setup time, and workplace safety. Aluminium dies can reduce weight by nearly 65% compared with comparable steel dies. The exact reduction depends on die size, geometry, inserts, and required strength. It is a useful engineering target, not a universal promise.
Lighter dies are easier to move between storage, inspection, and production areas. A small crane may complete a changeover with less lifting capacity. Operators can position the tool more accurately, reducing alignment mistakes. Faster handling also helps manufacturers respond to shorter production runs. Practical die-shop experience shows that these gains become noticeable during frequent tool changes.
The trade-off deserves honest attention. Aluminium usually wears faster than hardened steel in severe forming conditions. It can also expand more under heat, affecting precision during long production cycles. Engineers should check load, temperature, surface treatment, and expected service life before approval. In some cases, steel inserts or reinforced sections provide a better balance. The 65% figure sounds impressive. It still requires validation through testing, measurement, and production feedback.
Why Choose Aluminium Dies for Global Manufacturing? - Tooling Efficiency: Aluminium Dies Can Reduce Weight by Nearly 65%
Reference comparison based on an identical die volume of 10,000 cm³. Values are representative engineering data; actual performance depends on alloy, design, heat treatment, and operating conditions.
| Performance Dimension |
Aluminium Alloy Die
Reference: 6061-T6 |
Tool Steel Die
Reference: P20-type steel |
Cast Iron Die
Gray cast iron |
Manufacturing Relevance |
| Typical density |
2.70 g/cm³ |
7.85 g/cm³ |
7.20 g/cm³ |
Lower density directly reduces die mass for the same geometry. |
| Mass at 10,000 cm³ |
27.0 kg |
78.5 kg |
72.0 kg |
Useful for easier handling, installation, and lower fixture loading. |
| Weight reduction versus tool steel |
65.6% |
Baseline |
8.3% |
Aluminium can reduce mass by nearly 65% compared with tool steel. |
| Weight reduction versus cast iron |
62.5% |
9.0% heavier than cast iron |
Baseline |
Lower lifting and transport requirements can simplify global production logistics. |
| Thermal conductivity at approximately 20°C |
Approximately 167 W/m·K |
Approximately 29 W/m·K |
Approximately 50 W/m·K |
Higher conductivity can support faster heat transfer and shorter thermal stabilisation times. |
| Elastic modulus |
Approximately 69 GPa |
Approximately 210 GPa |
Approximately 100–150 GPa |
Aluminium designs may require added section thickness or structural support to control deflection. |
| Typical machining consideration |
Generally easy to machine; chip evacuation and tool geometry remain important. |
Higher cutting forces and longer machining cycles are common. |
Good damping; abrasive particles may accelerate tool wear. |
Material selection should balance machining time, rigidity, wear, and expected production volume. |
| Best-fit production use |
Prototype tooling, low-to-medium volume runs, lightweight fixtures, and thermally responsive dies. |
High-wear applications and long production runs requiring high hardness and rigidity. |
Rigid, vibration-sensitive tooling where mass and damping are priorities. |
The optimal choice depends on cycle count, contact pressure, temperature, and wear conditions. |
Calculation note: Mass = density × volume. For the same 10,000 cm³ die volume, aluminium weighs 27.0 kg compared with 78.5 kg for tool steel, resulting in a calculated weight reduction of 65.6%.
Lifecycle Economics: Aluminium Recycling Uses About 95% Less Energy
Why Choose Aluminium Dies for Global Manufacturing?
Lifecycle Economics: Aluminium Recycling Uses About 95% Less Energy
Aluminium dies support efficient manufacturing because they combine low weight, thermal conductivity, and practical machinability. In die-making workshops, these properties can reduce handling effort and shorten cooling cycles. A lighter die may also lower transport emissions when components move between production sites.
The stronger economic argument appears at the end of the die’s service life. Recycling aluminium usually requires about 5% of the energy used to produce primary aluminium. That means roughly 95% less energy, although the exact saving depends on alloy quality, contamination, and collection systems. Clean offcuts, worn dies, and machining chips can return to the material stream instead of becoming costly waste.
This is not an automatic result. Mixed alloys can complicate sorting. Coatings, lubricants, and attached steel parts may require extra processing. Manufacturing teams should record alloy grades and separate scrap at the worksite. Small labels and dedicated bins make that process more reliable.
A lifecycle review should also include die durability, repair frequency, shipping weight, and recycling access.
Aluminium is not always the best choice for every temperature or pressure condition. That deserves honest evaluation.
Still, when production needs lightweight tooling and responsible material recovery, aluminium offers a measurable advantage. The benefit becomes clearer when procurement, engineers, and recyclers share the same material records.
 +86-13516964051


 CONTACT NUMBER
 CONTACT NUMBER